Peeled Stainless Steel Bar vs Cold Drawn Bar: Machining Guide
Compare peeled and cold drawn stainless steel bar by surface-removal route, machining allowance, dimensional control, inspection method and final CNC requirement.
In This Guide
- Quick answer
- What peeling changes
- What cold drawing changes
- Peeled, cold drawn and centerless ground serve different jobs
- Match the route to the machining problem
- Grade selection remains a separate decision
- Inspect the incoming bar before shipment
- RFQ wording examples
- Packing and length still affect the usable result
- Stock and trial-order boundaries
- Common ordering mistakes
- Sources and scope
- Send a machining-bar RFQ
Peeled and cold drawn stainless steel bars can both arrive with a bright metal surface, but they are not the same machining stock. Peeling removes the outside layer with cutting tools. Cold drawing reduces the section through a die and cold-works the material. Those routes leave different questions for the buyer: how much stock remains, what tolerance is supplied, how straight the bar is and whether the material condition suits the finished part.
This comparison is for CNC workshops, shaft makers and industrial buyers deciding the incoming bar condition before quotation. The material grade still comes from the drawing and service environment; this page deals with the processing route.
Quick answer
Choose peeled stainless steel bar when removal of the original hot-rolled surface and a controlled machining allowance matter more than final precision. Choose cold drawn stainless steel bar when the available drawn size, surface and dimensional consistency fit routine machining. Move to centerless ground bar when a measured diameter tolerance, roundness or surface finish is too tight to leave implicit.
| Starting-stock need | More likely route | Confirm before ordering |
|---|---|---|
| remove scale and the original outside layer before final turning | peeled bar | final peeled diameter, remaining allowance and acceptable surface indications |
| repeat parts from bright bar with steadier section size | cold drawn bar | diameter tolerance, straightness and mechanical condition |
| feed through a close collet or use near-finished shaft stock | centerless ground bar | h class or drawing tolerance, roundness, roughness and straightness |
| large stock removal after receipt | hot rolled or peeled route, depending on surface risk | starting diameter, defect-removal allowance and machining yield |
No finish name replaces the drawing. `Bright`, `peeled`, `cold drawn` and `ground` need measurable dimensions beside them.
What peeling changes
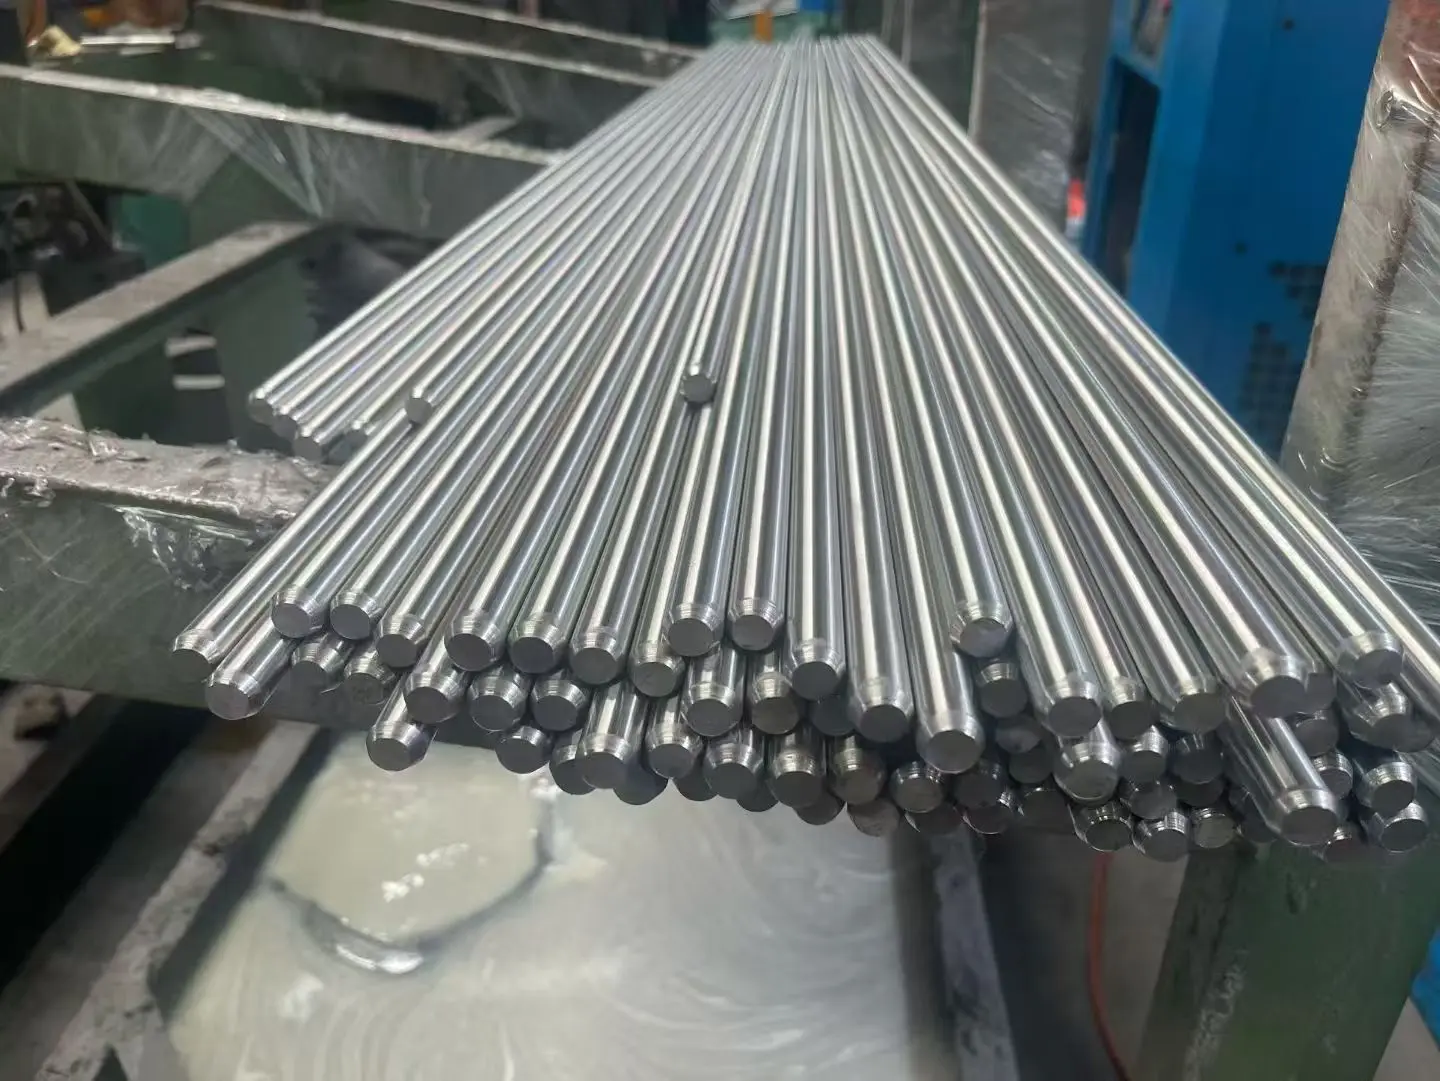
A bar-peeling machine removes a continuous layer from the outside of round bar with a rotating cutter head as the bar advances. The route removes scale and can remove shallow surface discontinuities from the original hot-worked surface. It also establishes a cleaner diameter for later machining.
Peeling does not make every underlying indication disappear, and it does not automatically produce final shaft tolerance. The amount removed, incoming condition and inspection standard still matter. A buyer normally orders the finished peeled diameter and states the machining allowance required for the final part. Specifying an arbitrary peel depth without the finished geometry can create unnecessary metal loss.
The terms `peeled` and `turned` are sometimes grouped in quotations because both remove outside metal. The machines work differently: peeling uses a rotating cutter head around the advancing bar, while turning normally rotates the workpiece against a tool. When the production route matters, name it. When the result matters more, state diameter, tolerance, surface and allowance.
Our peeled stainless steel bar page covers the commercial supply route and current availability boundaries.
What cold drawing changes
Cold drawing pulls prepared bar through a die to reduce and control the cross-section. Compared with rough hot-rolled stock, the process can provide a cleaner surface and steadier dimensions. It also cold-works the material, so strength, hardness and ductility can differ from an annealed bar depending on reduction and any later heat treatment.
That last point is easy to miss. A buyer who only writes `304 bright bar` has not defined the mechanical condition, diameter tolerance or straightness. For a component sensitive to forming, welding or mechanical properties, put the required condition and test values on the drawing or PO and check them against the MTC.
Cold drawing is not an automatic h9 guarantee. The supplied tolerance depends on size, shape, reduction route, straightening and the agreed specification. Read the family-mill cold drawing guide for the production stages without repeating that full process here.
Peeled, cold drawn and centerless ground serve different jobs
The three routes are not a simple quality ladder. Each solves a different incoming-stock problem.
| Item | Peeled bar | Cold drawn bar | Centerless ground bar |
|---|---|---|---|
| Main operation | outside metal removed by cutting | section reduced through a die | outside diameter finished by grinding |
| Main buying reason | surface cleanup plus machining stock | dimensional consistency and bright supply | tighter diameter and smoother cylindrical surface |
| Typical downstream work | final turning or substantial OD machining | repeat CNC turning, forming or fabrication as specified | precision shafts, pins and collet-fed parts |
| Diameter control | state finished peeled diameter and tolerance | state the agreed drawn tolerance | state h9/h8 or the drawing tolerance when required |
| Mechanical effect | mainly material removal | cold work can change properties | limited stock removal; incoming condition still matters |
| Surface boundary | not automatically defect-free or ground | bright does not define roughness | ground does not automatically define straightness or end condition |
| Cost question | does surface cleanup save later turning time? | does the drawn route meet the part without extra precision finishing? | is tighter incoming control worth the added grinding cost? |
A common route for demanding shaft stock is to use drawn or peeled incoming material and then grind to the final supply diameter. That does not mean every peeled or cold drawn order includes grinding. The sequence belongs in the PO.
Match the route to the machining problem
At quotation stage, four questions usually separate the routes faster than a long application list.
Will the machine remove the full outside diameter?
If the part will be turned across its full length, peeled stock may provide a cleaner and more predictable starting surface. The finished peeled diameter still needs enough stock for final turning, including any straightness or ovality allowance.
Does the bar feed through a collet or automatic lathe?
A bar feeder makes diameter consistency and straightness visible immediately. Cold drawn stock may suit routine feeding, but close collets or high spindle speed can expose small variations. Put the actual diameter and straightness limits on the drawing instead of relying on `bright bar`.
Is the incoming diameter close to the finished shaft size?
Near-net shaft stock leaves little room to remove size variation or surface marks. This is where centerless ground bar often becomes the clearer route. The h9, h10 and h11 guide explains the diameter classes; straightness and roughness remain separate fields.
Does the drawing control mechanical condition?
Cold work can affect reported mechanical properties. If hardness, tensile strength, yield strength or elongation matters, state the required condition and test basis. Peeling or grinding changes the surface geometry but does not replace grade and heat-treatment control.
Grade selection remains a separate decision
Processing route cannot repair a wrong grade choice. A peeled 303 bar and a cold drawn 316L bar differ in chemistry before the finishing route is considered.
- 303 stainless steel bar often enters repeat CNC work when chip control matters. Its corrosion margin is not the same as 304.
- 304/304L stainless steel bar covers broad industrial use, but 304L or dual certification needs support from the actual MTC.
- 316/316L stainless steel bar adds molybdenum-bearing chemistry for chloride-sensitive applications, without guaranteeing performance in every crevice or process medium.
Match the grade, standard and Heat Number first. Then decide whether peeling, drawing or grinding gives the machine the right starting stock.
Inspect the incoming bar before shipment
An inspection report needs values and locations, not only `size OK`. Agree on the method before production.
1. Diameter: measure near both ends and at the middle. Take readings in more than one orientation to identify ovality. 2. Straightness: use the drawing method, such as a specified support span and dial-indicator reading. A visual roll test is useful screening but not a substitute for a numeric requirement. 3. Surface: inspect under agreed lighting and record seams, pits, cutter marks, scratches or handling damage against the acceptance wording. Brightness alone proves little. 4. Roughness: measure Ra or the named parameter when the drawing controls it. Do not infer roughness from `polished` or `ground`. 5. Length and ends: check fixed length, saw tolerance, burrs and end protection separately from diameter. 6. Traceability: match grade and Heat Number across the MTC, bundle labels and packing list.
PMI can help confirm alloy identity for critical 316L, duplex or mixed-grade shipments, but it does not measure diameter, straightness or mechanical condition.
RFQ wording examples
These examples show the fields buyers can copy. Replace the dimensions with the actual drawing.
Peeled stock for final turning
Please quote 304 stainless steel peeled round bar, ASTM A276, finished peeled diameter 52 mm, minimum final part diameter 50 mm, diameter tolerance and straightness per attached drawing, 3 m fixed length, MTC and Heat Number labels required, 1 MT, FOB China port.
Cold drawn stock for repeat CNC work
Please quote 303 stainless steel cold drawn round bar, ASTM A582, 20 mm diameter, tolerance h11, straightness 1 mm/m max, 3 m length, MTC required, 500 kg, destination Laem Chabang, Thailand.
Ground stock for a controlled shaft diameter
Please quote 316L centerless-ground round bar, 12 mm h9, Ra 0.8 µm max, straightness 0.5 mm/m max, 2 m cut length, MTC and packing photos required, 300 kg, destination Jebel Ali, UAE.
The tolerance, straightness and roughness values above are example buyer requirements, not default capability claims.
Packing and length still affect the usable result
A controlled bar can arrive damaged if the bundle allows impact, bending or label loss. We keep grade, Heat Number, diameter and length visible on the bundle and separate heats or grades in mixed shipments. Wrapping, strapping points and end protection depend on bar diameter, finish and cut length.
For Southeast Asia and Middle East orders, confirm the container before fixing full length. Straight 6 m bars do not fit through the normal loading route of a standard 20ft container because its internal length is below 6 m. Use a shorter cut length, a 40ft container or another agreed shipping plan.
Stock and trial-order boundaries
FX Stainless Steel holds `1,000+ tons` across the overall stainless steel bar range. This is not a claim that every peeled or cold drawn grade and diameter is in stock. Availability comes from the requested grade, finished size, route, tolerance, length and current heat.
Selected stock sizes can support an `MOQ of 100 kg`. Peeling, special drawing, grinding, fixed-length cutting or project testing may require a different minimum. Send the complete specification so we can distinguish an available stock route from a custom production route.
Common ordering mistakes
- treating peeled and turned as exact synonyms without defining the finished result
- asking for `bright bar` without a process route or measurable tolerance
- assuming cold drawn means h9
- using diameter tolerance as if it also controls straightness and roughness
- choosing peeled stock without enough remaining allowance for final turning
- paying for ground bar when the first machining operation removes the whole outside diameter
- checking the MTC but not matching its Heat Number to the physical bundles
- fixing 6 m length before confirming the container and unloading plan
Sources and scope
This guide describes purchasing and inspection differences; it does not replace the standard or the part drawing. Useful references include ASTM A484/A484M general requirements for stainless steel bars, billets and forgings and ISO 286-2 limits and fits. The applicable product standard may be ASTM A276, ASTM A582, ASTM A479, EN 10088-3, JIS G4303 or another project specification.
Use the edition named by the buyer or end user. Process capability, tolerance and acceptance criteria need written confirmation for the actual size and route.
Conclusion
Peeled bar is mainly a surface-removal and machining-stock decision. Cold drawn bar is a section-reduction and dimensional-consistency route that also changes the material condition. Centerless grinding is the clearer option when the incoming diameter and cylindrical surface need tighter control.
Start with the finished part, then work backward: final diameter, stock removal, tolerance, straightness, roughness and mechanical condition. That sequence gives the supplier enough information to quote the right bar instead of the nearest familiar name.
Frequently asked questions
Q. What is the main difference between peeled and cold drawn stainless steel bar?
A. Peeling removes metal from the outside of a round bar with cutting tools, mainly to clean the surface and establish a new diameter with machining stock remaining. Cold drawing pulls prepared bar through a die, reducing the section and improving dimensional consistency and surface condition while also cold-working the material.
Q. Is peeled stainless steel bar better than cold drawn bar for CNC machining?
A. Not in every job. Peeled bar suits parts that still need outside-diameter machining and benefit from removal of the original surface layer. Cold drawn bar suits repeat machining when its available size, surface, straightness and mechanical condition meet the drawing. Compare the incoming condition against the finished part rather than ranking one route as universally better.
Q. Does cold drawn stainless steel bar automatically meet h9 tolerance?
A. No. Cold drawing can improve dimensional consistency, but h9 is a specified shaft tolerance tied to nominal diameter. Confirm the actual size tolerance and inspection method. A centerless-ground route is often considered when the required diameter and surface control are tighter than the cold-drawn supply condition.
Q. Are peeled bar and turned bar the same product?
A. They are related metal-removal routes but not exact synonyms. Bar peeling normally uses a rotating cutter head around a bar moving through the machine. Turning normally rotates the workpiece against a cutting tool. Suppliers sometimes group the terms commercially, so the PO needs the final diameter, tolerance, surface and allowance instead of relying on the name alone.
Q. What information belongs in a peeled or cold drawn bar RFQ?
A. Send the grade, standard, starting diameter, required incoming condition, final part diameter, machining allowance, diameter tolerance, straightness, surface requirement, length, quantity, MTC needs and destination. Add hardness or mechanical-condition requirements when cold work or heat treatment affects the part.
Send a machining-bar RFQ
Send the grade, standard, starting and finished diameter, process route, machining allowance, tolerance, straightness, surface, length, quantity and destination through the stainless steel bar quote page. We will confirm the available peeled, cold drawn or ground route, MTC requirements, cutting and export packing before quotation.